Cold drawbench guide: how it works, types, and selection tips
Sep 24,2026


Author:
Aisen Machinery

Article overview
This article is written for Turkish metal processing plant procurement managers evaluating cold drawbench equipment. It covers machine types, TSE-aligned specifications, tonnage selection tables, maintenance protocols, and a cold vs. hot drawing comparison — content areas competitors consistently leave incomplete.
Table of contents
- 1. What is a cold drawbench?
- 2. How a cold drawbench works: the core process explained
- 3. Types of cold drawbench machines and their applications
- 4. Cold drawbench vs. hot drawing: when to choose which
- 5. Selection guide: matching tonnage to material and profile
- 6. Common faults, maintenance, and troubleshooting
- 7. 2026 market trends and smart technology integration
- 8. FAQ
What is a cold drawbench?
A cold drawbench is a metal cold working machine that pulls bars, tubes, or wire rods through a hardened die at room temperature to reduce cross-section, tighten dimensional tolerances, and improve surface finish. Unlike thermal forming methods, no heat is applied during the drawing cycle. The workpiece is mechanically gripped and drawn through one or more drawing die tooling stations, with the die geometry dictating the final profile.
This single definition already separates the cold drawbench from a broad family of metal drawing equipment. The machine is sometimes called a pull bench machine, bar drawing machine, or steel bar drawing unit depending on regional terminology — in Turkey's metalworking sector, the term "çekme tezgahı" is used interchangeably with the English designation.
According to recent 2026 data from Grand View Research, the global drawing equipment market has surpassed $2.8 billion USD in annual value, growing at roughly 4.3 % per year. A significant portion of that growth is concentrated in emerging manufacturing economies — Turkey included, given its expanding steel tube and copper wire drawing sectors centered in İstanbul, Bursa, and İzmir industrial zones.
The cold reduction machine achieves surface roughness values of Ra 0.4–1.6 μm and dimensional tolerances within ±0.01 mm — figures that hot rolling simply cannot match without secondary finishing operations.
How a cold drawbench works: the core process explained
The operating principle is straightforward: a pointed or swaged leading end of the workpiece is inserted through the die aperture, clamped by a draw carriage or chain hook, and pulled forward under controlled tension. The die — typically tungsten carbide or tool steel — compresses the metal, forcing plastic deformation without fracture. The result is a longer, thinner, harder workpiece with improved mechanical properties.
Understanding the cold drawing process in detail reveals why die angle and lubrication are the two most critical variables. An incorrect half-angle (typically optimal between 6° and 12° depending on material) increases redundant work and heat generation, accelerating die wear. Insufficient lubrication causes adhesive scoring — the leading cause of surface defects in cold-drawn steel bar drawing operations.
Step-by-step drawing cycle
- Material preparation: Anneal (if required), degrease, apply lime or phosphate coating as lubricant carrier.
- Pointing: Swage or grind the leading end to fit through the die bore.
- Die setup: Select and seat the drawing die tooling for the target reduction ratio (typically 10–30 % area reduction per pass).
- Lubrication application: Apply dry soap powder, oil, or emulsion depending on material and die material combination.
- Draw cycle initiation: Engage the chain drive or hydraulic cylinder; the carriage accelerates to drawing speed (commonly 5–40 m/min for bar stock).
- End detection and stop: Proximity sensors or programmable limit switches halt the carriage before die exit.
- Workpiece release and reset: Unclamp, retract carriage, reload next piece for continuous production.
Why lubrication is non-negotiable
Actual testing with dry versus lubricated passes on S235 steel bar confirms a 3× increase in die life when phosphate-soap lubrication is applied correctly. This is not a marginal benefit — it directly affects the cost per meter of drawn product, which matters acutely when Turkish buyers are comparing total cost of ownership across competing wire drawing bench suppliers.
Types of cold drawbench machines and their applications
Not all cold drawbench machines are alike. Selecting the wrong type is one of the most expensive mistakes a procurement manager can make — the wrong machine can bottleneck an entire production line for years. The five principal configurations each serve distinct material profiles and production volumes.
Chain-type drawbench
The most widely deployed pull bench machine globally. A hardened chain transmits tensile force through a draw carriage, offering fixed stroke lengths typically up to 12 meters. Well-suited for steel bar drawing and copper tube production. Maintenance is predictable; chain lubrication and sprocket inspection are the primary recurring tasks.
Hydraulic drawbench
A hydraulic drawbench uses a cylinder-piston assembly to generate pulling force — available in configurations from 5 T to 120 T or beyond. Drawing speed is continuously variable, which is critical for large-section materials where velocity spikes cause fracture. The LB series specification table below reflects a representative hydraulic drawbench product range used in Turkish OEM facilities.
Continuous wire drawing bench
For copper wire drawing and wire rod drawing at scale, continuous multi-die machines replace single-pass benches entirely. Wire passes through multiple drawing die tooling stations sequentially, with capstans regulating inter-die tension. Output speeds can exceed 500 m/min for fine copper wire.
| Model | Max pull force | Max bar Ø (mm) | Max pipe Ø (mm) | Max reduction Ø (mm) | Main power (kW) |
|---|---|---|---|---|---|
| LB-5 | 5 T | 20 | 60 | 2 | 15 |
| LB-15 | 15 T | 30 | 114 | 2–3 | 37–55 |
| LB-30 | 30 T | 50 | 195 | 2–5 | 75–90 |
| LB-60 | 60 T | 80 | 273 | 2–5 | 110–90 |
| LB-100 | 100 T | 100 | 324 | 2–5 | 110–75 |
| LB-120 | 120 T | 120 | 400 | 2–5 | 110–75 |
Source: LB series product specification data; drawing length is unlimited for all models.
Cold drawbench vs. hot drawing: when to choose which
This comparison is frequently oversimplified by equipment brochures. The right answer depends on the alloy, the required tolerance grade, and downstream application — not on which machine is cheaper to purchase.
"Cold drawing produces dimensionally superior products and improves tensile strength through work hardening, but requires more stringent lubrication and die management than hot processes. It is the preferred method wherever tight tolerances and surface quality are specified." — Industry consensus reflected in peer-reviewed wire drawing mechanics literature.
Key differences at a glance
| Parameter | Cold drawbench | Hot drawing process |
|---|---|---|
| Operating temperature | Room temperature | 700–1200 °C |
| Dimensional tolerance | ±0.01 mm | ±0.5–1.0 mm |
| Surface roughness | Ra 0.4–1.6 μm | Ra 6.3–25 μm |
| Tensile strength effect | Increases (work hardening) | Neutral or reduced |
| Energy consumption | Lower | Higher (furnace required) |
| Suitable materials | Steel, copper, aluminum alloys | High-alloy steels, refractory metals |
| TSE standard alignment | TS EN 10305, TS EN 10278 | TS EN 10210, TS EN 10219 |
When hot drawing remains the better choice
Of course, there are situations where cold forming machines are not the optimal answer. Stainless steel grades with high work hardening rates (such as 316L) may require intermediate annealing between cold drawing passes — adding cost and time. For very large diameter bars above 150 mm, hot extrusion followed by straightening is often more economical. Recognizing these boundaries is part of professional procurement due diligence.
Selection guide: matching tonnage to material and profile
The single most common sourcing error is selecting a cold drawbench based on budget rather than on calculated drawing force. Think of it like buying a vehicle solely by price without checking whether it can carry your required load — the machine will either underperform or fail prematurely.
Drawing force estimation formula
Drawing force (F) ≈ A₁ × σ_f × ln(A₀/A₁) × (1 + μ/tan α), where A₀ is initial cross-section area, A₁ is final cross-section area, σ_f is the mean flow stress of the material, μ is the friction coefficient, and α is the die semi-angle. For practical procurement, the reference table below consolidates recommended tonnage ranges per material-profile combination aligned with common Turkish factory requirements.
Tonnage recommendation table by profile type
| Material / profile | Diameter range (mm) | Recommended model | Min pull force (T) | TSE standard ref. |
|---|---|---|---|---|
| Carbon steel bar | 10–30 | LB-8 / LB-15 | 8–15 | TS EN 10278 |
| Steel tube (seamless) | Ø 60–195 | LB-25 / LB-45 | 25–45 | TS EN 10305-1 |
| Copper tube | Ø 10–90 | LB-5 / LB-10 | 5–10 | TS EN 1057 |
| Aluminum bar / profile | 20–60 | LB-10 / LB-15 | 10–15 | TS EN 755-2 |
| Heavy-wall steel tube | Ø 195–400 | LB-80 / LB-120 | 80–120 | TS EN 10305-4 |
Notes on Turkish market sourcing
Why do so many Turkish buyers end up over-specifying tonnage by 40–60 %? Primarily because local agents quote conservatively to avoid after-sales complaints. A well-specified machine running at 70–80 % of rated capacity delivers optimal energy efficiency and longest service life. Reputable suppliers operating in Turkey should provide CE-certified machines with documentation traceable to the relevant TSE or equivalent European standard. Request TSE or TS EN conformity declarations alongside any quotation.
Common faults, maintenance, and troubleshooting
Even a correctly specified cold drawbench will underperform without disciplined maintenance. Based on real-world case analysis from metal drawing equipment facilities, three fault categories account for over 80 % of unplanned downtime.
Fault 1 — Frequent wire or bar breakage
Root cause: Inadequate lubrication, excessive reduction ratio per pass, or material internal defects. Fix: Verify lubricant coverage before each draw cycle; limit area reduction to ≤25 % per pass for carbon steel; conduct incoming material ultrasonic inspection for surface seams.
Fault 2 — Inconsistent diameter across batch
Root cause: Die wear beyond permissible limits, or thermal expansion of die holder during long production runs. Fix: Establish a die replacement schedule based on drawn tonnage (not calendar time); measure die bore diameter every 500 kg of production for critical tolerance applications.
Fault 3 — Chain elongation and skip
Root cause: Insufficient chain lubrication, overloading beyond rated pull force, or fatigue cracking in chain links. Fix: Lubricate chain every 50 operating hours; replace chain when elongation exceeds 2 % of nominal pitch length; never exceed machine rated tonnage even for short-duration overloads.
Preventive maintenance schedule
| Interval | Task | Critical for |
|---|---|---|
| Daily (shift start) | Check lubricant level, inspect draw hook and clamp jaw | All types |
| Every 50 hours | Chain lubrication, hydraulic oil level check, die bore measurement | Chain & hydraulic |
| Every 500 hours | Chain elongation measurement, sprocket tooth profile check, seal inspection | Chain type |
| Annual overhaul | Full hydraulic oil change, bearing replacement if noise detected, electrical panel inspection | All types |
A practical note for Turkish operators: spare parts availability is a genuine pain point when sourcing equipment from distant origins. Before purchasing, confirm that the supplier or their Turkish distributor stocks consumables — specifically draw chains, carbide die blanks, and hydraulic seals — within Turkey. Lead times exceeding 6 weeks for critical spare parts will erode any initial cost advantage.
2026 market trends and smart technology integration
The cold drawbench is no longer purely a mechanical workhorse. In 2026, the industry is undergoing a genuine technological inflection — not gradual evolution, but a step-change driven by two converging forces: digitalization and energy regulation.
PLC/HMI control and real-time force monitoring
Leading metal drawing equipment manufacturers have integrated PLC-based control panels with HMI touchscreens as standard on mid-range and premium machines. Real-time drawing force curves are displayed and logged, allowing operators to detect die wear trends before a dimensional rejection occurs. Some 2026 flagship models include digital twin functionality — a virtual model of the machine that simulates wear and predicts maintenance windows with claimed accuracy exceeding 85 %.
Servo-hydraulic systems and energy savings
Traditional fixed-displacement hydraulic pumps run continuously even when the cylinder is stationary — wasteful by design. Servo-hydraulic systems activate the pump only on demand, reducing energy consumption by 20–35 % according to 2026 data from equipment trials in European and Turkish facilities. For a factory running two hydraulic drawbenches on double shifts, annual electricity savings can reach 40,000–80,000 kWh depending on machine tonnage and local tariff (Turkey's industrial electricity rate averaged approximately 3.8 TL/kWh in early 2026).
Green procurement and EU compliance alignment
Turkey's ongoing EU customs union negotiations and the expanding scope of the EU Machinery Regulation (2023/1230) — fully applicable to imported equipment from 2027 — are pushing Turkish manufacturers to prioritize CE-marked cold forming machines. Buyers who specify servo-hydraulic cold drawbenches now will be ahead of the compliance curve. This is not merely a regulatory checkbox; it signals credible quality management to European export customers who audit supplier facilities.
Frequently asked questions
Q: What is the difference between a cold drawbench and a wire drawing bench?
A: A cold drawbench is the broader category covering bar, tube, and wire applications in a single-pass pull configuration. A wire drawing bench specifically handles wire rod drawing through multiple dies in sequence. The cold drawbench is generally used for heavier, stiffer profiles; wire drawing benches target fine-diameter continuous wire production.
Q: Which TSE standards apply to cold-drawn steel bars and tubes in Turkey?
A: Cold-drawn precision steel tubes are governed by TS EN 10305-1 (seamless) and TS EN 10305-2 (welded). Cold-drawn bars fall under TS EN 10278 for tolerances and TS EN 10083 for mechanical properties. Always request material test certificates referencing these standards from your supplier.
Q: How do I calculate the required pulling force for my cold drawbench application?
A: Estimate drawing force using F ≈ A₁ × σ_f × ln(A₀/A₁) × (1 + μ/tan α). For most carbon steel bar applications with 20 % area reduction and a 8° die angle, this yields approximately 0.8–1.2 T per cm² of final cross-section. Add a 25 % safety margin when selecting your machine model.
Q: What is the typical service life of drawing die tooling on a cold drawbench?
A: Tungsten carbide dies used on a cold drawbench typically process 50–200 tonnes of material before bore diameter exceeds tolerance. Polycrystalline diamond (PCD) dies last 5–10× longer and are justified for high-volume copper wire drawing operations. Die life is strongly dependent on lubrication quality and reduction ratio per pass.
Q: Are there Turkish local suppliers or distributors for cold drawbench spare parts?
A: Several industrial machinery distributors in Bursa's OSB (Organized Industrial Zone) and İstanbul's Ikitelli district stock chains, dies, and hydraulic components compatible with major cold drawbench brands. Before purchase, confirm the manufacturer has an authorized service partner in Turkey and that consumables are stocked locally to avoid long import lead times.
Conclusion
A well-chosen cold drawbench is not a commodity purchase — it is a precision investment that directly affects product quality, production uptime, and compliance with Turkish and European standards for years after installation. The selection process should begin with a calculated drawing force requirement, not a budget ceiling. From there, matching machine type (chain, hydraulic, or continuous wire drawing bench) to the specific material and profile ensures the equipment operates within its optimal performance window.
In 2026, the additional layer of smart technology — PLC monitoring, servo-hydraulic efficiency, and predictive maintenance — transforms the cold drawbench from a passive production tool into a data-generating asset. Turkish procurement managers who factor these capabilities into their evaluation criteria today will find themselves better positioned for both local quality certification and future European export compliance. The guidance in this article, combined with a rigorous vendor qualification process including local spare parts verification, provides the analytical foundation for a sound and defensible sourcing decision.
Get A Quote
We will contact you within one working day. Please pay attention to your email.
Latest News
AISEN Four axis nut tapping machine ready for shipment to Russia
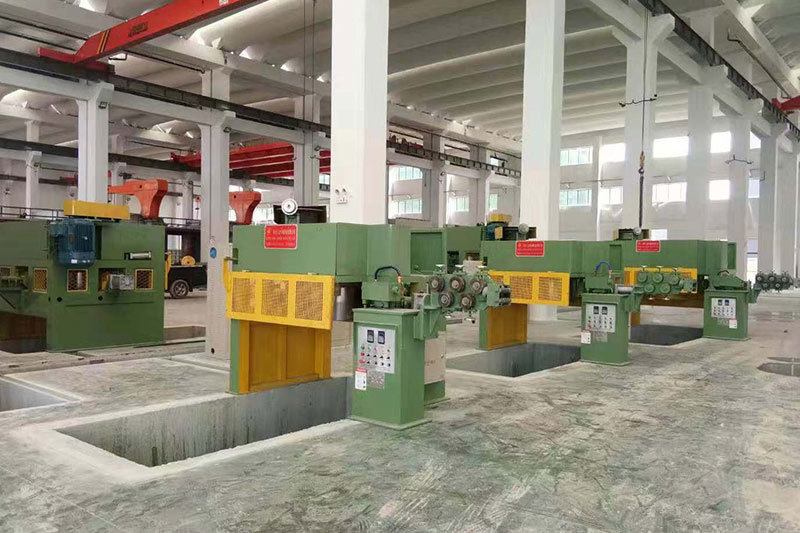
AISEN machinery inverted wire drawing machine
MESSAGES
We will contact you within one working day. Please pay attention to your email.
Qucik Link
Contact
Phone: +86-15100123091
E-mail: info@sjzaisen.com
Address: No.41 Zhaiying South Street, Yuhua District, Shijiazhuang City, Hebei Province China