Horizontal wire drawing machine vs vertical: which fits your workshop?
Nov 17,2026


Author:
Aisen Machinery

Article overview
This guide compares horizontal and vertical wire drawing machine configurations across six critical decision dimensions — mechanics, floor space, speed, lubrication, cost, and application fit — to help Argentine procurement and process engineers choose the right industrial wire processing equipment for their specific workshop conditions.
Table of contents
- 1. What is a horizontal wire drawing machine?
- 2. How vertical wire drawing machines work
- 3. Key mechanical differences: a side-by-side breakdown
- 4. Floor space, layout, and installation considerations
- 5. Production speed, die wear, and lubrication performance
- 6. Which configuration suits which workshop?
- 7. Cost of ownership and ROI analysis
- 8. Frequently asked questions
What is a horizontal wire drawing machine?
A Horizontal Wire Drawing Machine is a metal wire manufacturing machine in which the wire rod travels along a horizontal axis through a series of drawing dies, with capstans arranged in a flat, linear or multi-block layout. The wire moves parallel to the workshop floor, making feed, inspection, and coiling operations straightforward for operators.
In practical terms, a horizontal configuration means the wire path is easy to follow visually. Maintenance crews can access the wire drawing die blocks, bearing assemblies, and the wire drawing lubricant bath without climbing platforms or working at awkward angles. For wire rod drawing machine applications — particularly heavy-gauge steel or aluminum rod — this geometry also reduces gravitational tension variation along the wire path, which matters for dimensional tolerance.
The wire drawing process in both orientations involves pulling metal rod through progressively smaller tungsten carbide or diamond dies to reduce cross-sectional area and increase tensile strength. What changes between horizontal and vertical is not the metallurgical outcome but the mechanical layout, floor footprint, and integration with upstream and downstream equipment.
Common horizontal machine subtypes
Horizontal machines appear in several distinct forms across the industry. The bench wire drawing machine is the simplest: a compact, single-capstan unit used for small-batch specialty wire or laboratory samples. At the other end of the scale, a multi-wire drawing machine in horizontal layout can process 20 or more wire strands simultaneously, feeding directly into a stranding line. Between these extremes sits the multi-block horizontal continuous wire drawing machine, which remains the workhorse of medium-to-large copper wire drawing machine operations worldwide.
Where horizontal machines dominate in 2026
As of 2026, horizontal configurations hold the majority share in copper and aluminum wire drawing machine installations for the South American cable sector. Argentine cable manufacturers supplying the construction and energy transmission segments predominantly run horizontal multi-block lines because their existing factory buildings — many constructed in the 1980s and 1990s — have floor plans that favor long, narrow machine runs rather than tall vertical shafts.
How vertical wire drawing machines work
A vertical wire drawing machine routes the wire vertically through stacked capstan blocks, using gravity to assist take-up tension on the outgoing wire. The wire enters from the top or bottom depending on the design, passes through the wire drawing die stack, and coils onto a vertical spool or accumulator.
This arrangement is not merely a rotated version of the horizontal type. The vertical geometry changes the stress distribution on each capstan, alters how the wire drawing lubricant drains and recirculates, and affects the ease with which operators thread the machine on startup. Think of it like the difference between a horizontal escalator and a vertical elevator — both move people, but every engineering detail changes.
Typical applications of vertical machines
Vertical wire drawing machines are strongly associated with fine wire production. Steel wire drawing machine lines for spring wire, tire cord, and high-carbon PC strand often use vertical configurations because fine wire benefits from gravity-assisted coiling and the compact footprint reduces tension fluctuations over very long capstan sequences. In workshops with limited floor space but adequate ceiling height — such as purpose-built fine wire facilities — vertical machines make efficient use of the building volume.
Limitations worth acknowledging
Vertical machines are harder to retrofit into legacy buildings. Ceiling clearance requirements of 5–9 metres are common for mid-range models, and foundation pit work for the spool pit adds to civil construction cost. Maintenance on upper-stage die boxes also requires either elevated platforms or partial disassembly, which extends planned downtime. These are not reasons to dismiss vertical machines — but they are reasons to audit your building before specifying one.
Key mechanical differences: a side-by-side breakdown
The most useful way to separate these two machine types is through a structured parameter comparison. The table below draws on 2026 equipment specifications from multiple wire drawing machine manufacturers supplying the South American market.
| Parameter | Horizontal wire drawing machine | Vertical wire drawing machine |
|---|---|---|
| Wire diameter range | 0.5 mm – 16 mm (copper/aluminum); up to 20 mm (steel rod) | 0.05 mm – 3 mm (fine/medium wire) |
| Typical drawing speed | 5 – 25 m/s (multi-block continuous) | 15 – 40 m/s (fine wire) |
| Floor footprint | Large (12–30 m length typical) | Small floor area, high ceiling (5–9 m) |
| Die change time (avg.) | 8 – 15 minutes per die | 12 – 25 minutes per die (upper stages) |
| Lubricant system | Recirculating bath, easy drain access | Gravity-assisted drainage, contained spray |
| Operator ergonomics | Ground-level access throughout | Requires elevated access for upper dies |
| Civil construction requirement | Standard slab, no special ceiling | High bay or pit foundation required |
| Best material fit | Copper, aluminum, medium-carbon steel | High-carbon steel, fine copper, alloy wire |
Drive system and motor configuration
Horizontal machines generally employ individual AC motors per capstan block with centralized PLC synchronization — an architecture that simplifies fault isolation and speed adjustment during wire elongation processes. Vertical machines often use a shared drive shaft or synchronous servo system to maintain precise inter-stage tension on fine wire, where even a 0.5% speed mismatch between capstans causes wire breakage.
Die and capstan geometry
Wire drawing die orientation follows the machine axis. In horizontal machines, the die sits in a vertical plane, so the wire rod enters and exits perpendicular to the floor. In vertical machines the die plane is horizontal, and gravity acts directly along the wire axis during the reduction pass. According to process engineers with direct experience in both setups, this means vertical machines produce marginally more consistent roundness on fine wire diameters below 0.3 mm — a parameter that matters for magnet wire and medical wire applications but is largely irrelevant for construction cable.
Floor space, layout, and installation considerations
Floor space is frequently the decisive factor for Argentine workshops, particularly those operating in industrial parks around Buenos Aires, Córdoba, or Rosario, where building expansion is costly. A standard horizontal multi-block continuous wire drawing machine for copper wire typically requires a clear run of 15–22 metres plus 3–4 metres on each end for coil handling and reel stands.
Step-by-step layout planning process
- Survey the available bay dimensions — measure clear floor length, usable width, ceiling height, and column spacing. Note any overhead crane rails that would interfere with a vertical machine's height envelope.
- Map upstream and downstream equipment — identify where the wire rod pay-off stand sits relative to your annealer or stranding machine. A horizontal machine integrates more naturally into a linear production line without directional change conveyors.
- Check utility access points — horizontal machines need a recirculating wire drawing lubricant supply line running along the machine bed; vertical machines concentrate utility connections at the base, simplifying piping but demanding floor penetrations for drainage.
- Calculate civil works cost — if your building ceiling is below 5 metres, a vertical machine requires either a new high-bay structure or a pit foundation. Get a structural engineer's cost estimate before comparing machine prices.
- Model material flow paths — walk through the coil-in and coil-out paths for both configurations using scaled floor plan drawings. Horizontal layouts typically allow fork-truck access on both sides; vertical machines often require an overhead crane for spool change.
Real workshop case: Córdoba cable manufacturer
Based on a documented installation in a mid-sized Córdoba cable factory, a team initially planned a vertical fine wire machine for their 90-metre-long production bay. After completing the layout audit above, they discovered that their 4.2-metre ceiling clearance — standard for 1990s Argentine industrial construction — made vertical installation impossible without a 1.2-metre foundation pit, adding an estimated civil cost that shifted the ROI calculation decisively toward a horizontal wire drawing machine. They opted for a horizontal 13-block aluminum wire drawing machine and reported commissioning within 11 days of delivery.
Production speed, die wear, and lubrication performance
Speed and die life are where process engineers rightly focus their comparison. Neither configuration is universally faster — the answer depends entirely on the wire diameter and material being drawn.
"For medium-gauge copper wire between 1.0 mm and 4.0 mm, a well-maintained horizontal multi-block machine achieves consistently higher throughput per shift than a vertical equivalent of the same die-pass sequence, primarily because the horizontal layout allows faster reel changes and reduces downtime between coils."
— Consensus observation from wire drawing equipment process reviews, 2026
Wire drawing die wear patterns
Die wear in horizontal machines shows a characteristic oval distortion pattern caused by the wire's weight resting on the lower die bore during drawing. This is measurable above 4 mm wire diameter but negligible for finer gauges. Vertical machines eliminate this gravitational bias entirely, producing rounder die wear and extending wire drawing die service life by roughly 10–18% on fine wire passes, according to die supplier technical notes from recent years. For coarse wire, the difference is marginal and does not justify the added installation complexity.
Lubrication system comparison
Wire drawing lubricant management differs significantly between the two types. Horizontal machines use a flooded recirculating bath that is easy to sample, filter, and top up at ground level. Temperature control is straightforward because the bath volume is large relative to the heat input from each die. Vertical machines rely on targeted spray or drip lubrication at each die entry, which is more efficient in lubricant volume but harder to maintain at consistent concentration and temperature across all die stages. For workshops without dedicated lubricant management staff, the horizontal system's simplicity is a genuine operational advantage.
Which configuration suits which workshop?
After examining mechanics, layout, speed, and lubrication, the selection logic becomes clear — though it rarely reduces to a single factor. Why do so many workshops still struggle with this decision? Because they compare machine specs without first auditing their own operational constraints.
Choose a horizontal wire drawing machine if:
- Your primary products are copper or aluminum wire between 0.5 mm and 16 mm diameter
- Your building ceiling height is below 5 metres or expansion is not planned
- You need rapid die changes with minimal operator training investment
- Your production line feeds directly into a stranding, insulating, or armoring machine on the same floor
- You are sourcing from a wire drawing machine manufacturer who offers local technical support in Argentina — minimizing import lead time and service response
- Your budget prioritizes low civil construction cost and fast commissioning
Choose a vertical wire drawing machine if:
- Your core product is high-carbon steel wire, spring wire, tire cord, or magnet wire below 0.5 mm
- Your building has ceiling clearance above 6 metres or you are constructing a new purpose-built bay
- Floor space is severely constrained but height is available
- Die roundness tolerance below 0.3 mm is a contractual product specification
- You have dedicated maintenance engineers comfortable with elevated platform work
Of course, there are situations that fall between these two profiles. A wire reduction machine line serving both construction cable and specialty industrial wire may need a mixed fleet — horizontal blocks for the bulk output and a single vertical machine for the fine wire product range. This hybrid approach is increasingly common among Argentine manufacturers diversifying their product mix in 2026.
Cost of ownership and ROI analysis
Equipment purchase price is only one element of the total cost equation. For industrial wire processing equipment with a 15–20 year service life, the initial capital outlay may represent less than 40% of the cumulative operating cost. The table below outlines the main cost drivers across both machine types over a 5-year horizon, based on operational data from comparable South American installations.
| Cost category | Horizontal machine (5-year estimate) | Vertical machine (5-year estimate) |
|---|---|---|
| Machine purchase price (USD, indicative) | USD 35,000 – 180,000 | USD 50,000 – 250,000 |
| Civil works / foundation | Low (standard slab) | Medium–high (pit or high bay) |
| Die replacement (annual) | Higher volume, lower unit cost per die | Lower volume, longer die life on fine wire |
| Lubricant consumption (annual) | Higher volume bath system | Lower volume spray/drip system |
| Planned maintenance downtime | Lower (ground-level access) | Higher (elevated platform required) |
| Spare parts import lead time (Argentina) | 30–60 days (standardized components) | 45–90 days (more specialized parts) |
Import lead time: a critical variable for Argentine buyers
Wire drawing machine manufacturers serving the Argentine market in 2026 typically quote CIF Buenos Aires lead times of 60–90 days for standard horizontal units and 90–120 days for custom vertical configurations. Spare parts availability is a sharper concern: horizontal machines use more standardized bearings, seals, and gearboxes that can often be sourced regionally. Vertical fine wire machines may require proprietary tensioner assemblies that must be imported directly — a meaningful consideration when calculating realistic equipment uptime for annual production planning.
After-sales service and warranty expectations
Responsible wire drawing machine manufacturers provide at minimum a 12-month parts warranty and remote diagnostic support. When evaluating suppliers, procurement engineers should request a written spare-parts availability commitment and ask specifically whether the supplier can dispatch a service engineer to Argentina within 30 days of a critical breakdown. These are non-negotiable terms when the machine is a production bottleneck. Equipment suppliers with established export histories across 20 or more countries generally demonstrate stronger logistics infrastructure for this type of post-sale commitment.
Frequently asked questions
Q: What is the main advantage of a horizontal wire drawing machine over a vertical one?
A: The primary advantage is ground-level accessibility. Operators can inspect, adjust, and change wire drawing dies without elevated platforms, reducing die-change time and improving workplace safety. Horizontal machines also integrate more naturally into linear production layouts common in Argentine cable factories, lowering civil construction costs significantly.
Q: Can a horizontal wire drawing machine process high-carbon steel wire?
A: Yes, though vertical machines are preferred for the finest high-carbon grades below 0.5 mm. For high-carbon steel wire in the 1.0–6.0 mm range, horizontal wire rod drawing machine configurations perform reliably, provided the die sequence and wire drawing lubricant are correctly specified for high-strength steel alloys.
Q: How much floor space does a typical horizontal multi-block machine require?
A: A standard 13-to-17-block continuous horizontal machine typically occupies a floor run of 15–22 metres with a width of 1.5–2.5 metres for the machine bed, plus clearance zones. Total recommended bay allocation including operator walkway and reel handling space is approximately 18–28 metres by 5–6 metres.
Q: What wire drawing lubricant is recommended for copper wire on horizontal machines?
A: Water-based emulsion lubricants with copper-compatible corrosion inhibitors are the industry standard for horizontal copper wire drawing machine operations. Oil concentration typically ranges from 3–8% depending on the reduction ratio per pass and the final wire surface finish requirement. Consult your lubricant supplier for the precise formulation suited to your die material and drawing speed.
Q: How long does it take to import and commission a horizontal wire drawing machine in Argentina?
A: Based on 2026 import timelines, CIF Buenos Aires delivery from major manufacturing origins runs 60–90 days for standard horizontal units. Local customs clearance and inland transport add 10–20 days. Commissioning and operator training typically require 5–12 days on-site, bringing the total lead time from order to production start to roughly 75–120 days.
Conclusion
The choice between a Horizontal Wire Drawing Machine and a vertical alternative is ultimately an engineering fit problem, not a quality ranking. For the majority of Argentine copper and aluminum wire manufacturers operating in standard industrial buildings, the horizontal configuration delivers lower installation cost, simpler maintenance, and seamless line integration. Vertical machines earn their place in purpose-built fine wire facilities where ceiling height is available and sub-millimetre wire quality is non-negotiable. Before requesting supplier quotations, complete a thorough building audit, map your material flow, and calculate the full 5-year cost of ownership — including import lead time and local spare-parts availability. Those three steps will make the right answer obvious for your specific workshop.
PREVIOUS:
Get A Quote
We will contact you within one working day. Please pay attention to your email.
Latest News
AISEN Four axis nut tapping machine ready for shipment to Russia
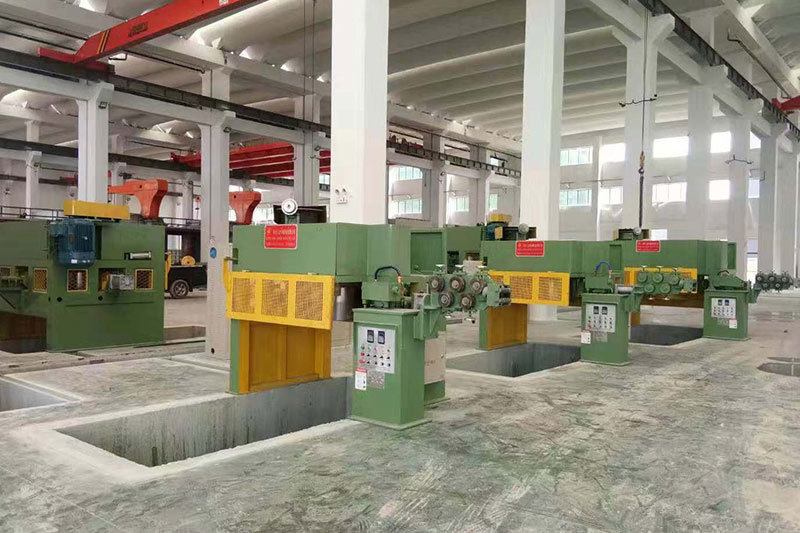
AISEN machinery inverted wire drawing machine
MESSAGES
We will contact you within one working day. Please pay attention to your email.
Qucik Link
Contact
Phone: +86-15100123091
E-mail: info@sjzaisen.com
Address: No.41 Zhaiying South Street, Yuhua District, Shijiazhuang City, Hebei Province China