Progressive header cold heading machine: die stages, tonnage, and wire diameter
Nov 13,2026


Author:
Aisen Machinery

Article overview
This article breaks down how a progressive header cold heading machine is selected in practice: how many die stations a part needs, how tonnage is matched to blank diameter, and how wire diameter and material limit what one frame can run. It also covers Argentina-specific procurement points - landed cost, import logistics, local technical support, and acceptance standards - that most English-language buying guides skip entirely.
Table of contents
- 1. What a progressive header cold heading machine actually does
- 2. Die stages explained: from wire to finished head
- 3. Tonnage selection: matching press force to part geometry
- 4. Wire diameter and material range
- 5. Cold heading vs hot heading vs machining: a decision matrix
- 6. Argentina market: pricing, TCO, and import logistics
- 7. Operational data: die life, changeover, energy, and maintenance
- 8. Procurement checklist: RFQ, acceptance, and after-sales terms
What a progressive header cold heading machine actually does
A progressive header cold heading machine forms a fastener blank through several die stations in one continuous stroke. Wire feeds in, a cut-off blade sizes the blank, and each station - working cold, without heating the metal - pushes it one step closer to the finished bolt, screw, or rivet head. This is the defining trait of cold heading technology: the metal grain flows around the shape instead of being cut away, which is why headed fasteners generally hold up better under cyclic load than machined equivalents of the same alloy.
Inside a fastener production line, this press usually sits right after wire drawing and right before thread rolling, as part of the broader fastener manufacturing process. It's not simply a cold forming machine that strikes once - it's a multi-station cold header where each blow does a specific, smaller job. Some first-time buyers still confuse the two categories at quotation stage. Why does that distinction matter so much? Because a single-blow press cannot build the layered head geometry modern fasteners need, while a progressive header cold heading machine can, and the price difference between the two usually reflects exactly that gap in capability.
What makes it different from a simple cold forming machine?
A basic cold forming machine typically has one or two stations and handles simple shank work with a flat or slightly domed head. A progressive header cold heading machine runs four, five, or six stations in sequence, each die performing a partial upset rather than one heavy blow. Shop-floor experience on hex flange bolt lines shows that moving from a two-die to a five-die layout lets a plant form a washer face directly during heading, removing a secondary machining operation and the scrap it generates. The trade-off is tooling cost and setup complexity, which is exactly why tonnage and station count need to be specified together, not separately.
Where does it fit in a fastener production line?
Positioned between wire straightening and thread rolling, this machine is the backbone of most fastener manufacturing equipment layouts, and it is rarely a standalone decision. Upstream, wire diameter tolerance and surface lubrication are controlled closely; downstream, the headed blank moves to thread rolling, heat treatment, or plating. Treating the header as an isolated purchase, instead of sizing it against the rest of the line, is one of the most common and costly planning mistakes a plant can make - a bottleneck anywhere else in the line will waste the header's full capacity.
Die stages explained: from wire to finished head
Each die stage on a progressive die forming machine removes one degree of freedom from the blank's final shape, moving it gradually from a straight wire segment toward the finished geometry. The first station cuts and centers the blank; the middle stations upset the head volume step by step; the last station finishes the head face, chamfer, or drive recess. Asking one die to do two jobs at once is the fastest route to a cracked head or torn grain flow, which is why station count is never just a cost-cutting variable.
How many stations does a progressive header cold heading machine need?
Most plants run four to six stations in practice. A simple hex bolt may need only four: cut-off, first upset, second upset, and trim. A flange bolt with a formed washer face, or a socket cap screw with a deep recess, usually needs five or six stations because the extra head volume has to move in smaller, safer increments. Industry consensus among tooling engineers is that adding a station reduces stress per blow and extends die life, even though it slightly slows the stroke rate - a trade worth making on high-volume parts, less so on short runs.
What happens at each stage, from wire to head?
- Wire feed and straightening from the coil.
- Cut-off to length, sized against target blank volume.
- First upset, rough-forming the head volume.
- Second upset, bringing the head closer to final diameter.
- Finish strike, forming chamfer, flange, or drive recess.
- Ejection and transfer to the trim or thread-rolling station.
This sequence is what separates a true multi-station cold header from a basic bolt making machine that only handles the shank. Getting the station count wrong at the quotation stage - usually by under-specifying it to save on tooling cost - is a recurring, and genuinely expensive, mistake once the line is running at volume.
Tonnage selection: matching press force to part geometry
Tonnage on a progressive header cold heading machine is set by blank diameter, material strength, and how much the final station upsets in one blow - not by wire diameter alone. A 100-ton press and a 250-ton press can both run 8mm wire, yet produce very different head sizes depending on die design and how the forming load is split across stations.
How do you calculate tonnage for a given bolt diameter?
Shops commonly estimate required force from blank cross-section area multiplied by the material's flow stress at forming temperature, then add a safety margin for the last, heaviest upset station. In practice, engineers rarely trust the formula alone; they confirm it with a trial strike and inspect the finished head for flash or incomplete fill before locking in the die design. A high speed cold header running light, low-carbon wire needs noticeably less tonnage than the same frame forming medium-carbon steel at the same diameter, so material grade belongs on the RFQ from day one.
What tonnage range covers most fastener plants?
Based on typical machine builder catalogs and common shop practice, small-diameter work (M3-M8) runs on 60-150 ton frames, mid-range bolts (M8-M16) need 150-350 tons, and heavy fasteners above M16 often require 350-600 ton metal forming press frames. Buying more tonnage than the part needs wastes energy and floor space; buying too little shortens die life and risks frame damage over time, which costs far more than the tonnage upgrade would have.
| Wire diameter | Typical bolt range | Tonnage band | Common stations |
|---|---|---|---|
| 2.5-6 mm | M3-M6 | 60-120 tons | 3-4 |
| 6-10 mm | M6-M10 | 120-220 tons | 4-5 |
| 10-16 mm | M10-M16 | 220-350 tons | 5-6 |
| 16-24 mm | M16-M24 | 350-600 tons | 5-6 |
Wire diameter and material range
Wire diameter capacity on a progressive header cold heading machine usually spans 2mm to 24mm across a manufacturer's model line, though no single frame covers that whole band - each model is built around a narrower window, matched to its tonnage and stroke length.
What wire diameter can a high speed cold header handle?
Light, high-speed frames aimed at small fasteners typically handle 2-8mm wire at 200-400 strokes per minute. Larger frames built for structural bolts slow down to 60-120 strokes per minute but handle 10-24mm stock. Pushing wire diameter near the top of a frame's rated range tends to shorten die life, something shop supervisors usually notice within the first few thousand cycles if tonnage was undersized at quotation to win the order on price.
Which materials work best with cold forging machine dies?
Low-carbon and medium-carbon steel wire are the most common feedstock, alongside stainless grades like 304 and 316 and, for lighter fasteners, aluminum. Boron steel is increasingly used for high-strength bolts, but it work-hardens faster and demands more frequent die inspection than plain carbon steel. A wire forming machine feeding inconsistent coil diameter - more than roughly ±0.05mm variance - is one of the most overlooked causes of head cracking, even when tonnage and die design are correct on paper. Nut forming machine lines and screw making machine lines share the same wire-handling logic, though nut blanks are usually pierced rather than headed, which changes the die stack entirely and should never be quoted against the same tooling.
Cold heading vs hot heading vs machining: a decision matrix
Choose cold heading for standard bolts, screws, and rivets up to roughly 24mm in common steel and stainless grades; choose hot heading for very large or low-ductility alloys; choose machining for short runs or complex, non-rotationally-symmetric parts. That is the short answer - the fuller picture depends on volume, tolerance, and part geometry, and whether the output is a bolt, a screw, or a rivet forming machine product rarely changes which column of the decision matrix applies.
When should you choose hot heading instead?
Hot heading makes sense when the blank diameter is large, the alloy has low cold ductility, or the head geometry demands more material flow than cold dies can safely achieve in a few stations. It costs more per piece in energy and tooling wear, so most plants reserve it for parts a cold forging machine genuinely cannot form without cracking the head or tearing the grain structure.
When is machining still the better option?
For prototype runs, very low volumes, or asymmetric special parts, CNC machining remains more economical than building dedicated progressive die forming machine tooling. The breakeven point, based on common shop-floor experience, usually sits somewhere between 5,000 and 20,000 pieces - below that, tooling cost per part on a header is hard to justify; above it, cold heading wins decisively on cycle time and material yield.
| Criteria | Cold heading | Hot heading | Machining |
|---|---|---|---|
| Typical volume | High, 20,000+ pcs | Medium-large diameter runs | Low, prototype to 5,000 pcs |
| Material yield | High, minimal waste | Moderate | Low, chips removed |
| Grain flow strength | Strong, continuous | Strong | Interrupted by cutting |
| Tooling cost | Moderate upfront | High | Low per job, high per part at volume |
As general metalworking references note, preserving continuous grain flow during cold forming techniques is a key reason headed fasteners resist cyclic and shear loads better than machined parts cut from the same alloy.
Argentina market: pricing, TCO, and import logistics
A progressive header cold heading machine suited to small and mid-range fasteners generally lands in the USD 25,000-90,000 range ex-works, with heavier structural-bolt frames running higher; the final landed cost for an Argentine buyer depends heavily on import duty, freight, and exchange-rate timing, not just the machine price tag on the quotation.
What price range should Argentine buyers expect?
Beyond the ex-works figure, plants should budget for ocean freight, port handling, and Argentina's import tariff schedule for capital goods, which can add a meaningful percentage on top of the base machine cost. Currency timing matters too - locking a price while negotiating payment terms in a stable currency, then converting close to shipment, is a common way local buyers manage exchange-rate exposure on a six-figure capital purchase.
How do import tariffs and logistics affect total cost?
Total cost of ownership should also include inland transport from the port, installation and commissioning labor, spare parts (repuestos) stock, and operator training time. A machine quoted 15% cheaper but lacking a documented asistencia técnica network in South America can end up costing more once the first die breaks and no local support is available to diagnose it quickly. For Spanish-speaking engineering teams, confirming that technical documentation and quotation terms - encabezadora progresiva, trefilado, remachadora - are available bilingually avoids costly misunderstanding at the installation stage, well before the first production run even starts.
Operational data: die life, changeover, energy, and maintenance
Die life, changeover time, and energy draw are the three numbers that decide real cost per piece on a progressive header cold heading machine, more than the headline tonnage figure ever does on its own.
How long do progressive dies last before replacement?
Under normal duty with correctly sized tonnage, header dies commonly run 200,000 to 1,000,000 strokes before resharpening, depending on wire hardness and station load. Finish-stage dies, carrying the heaviest upset, wear first and are usually swapped two to three times more often than the cut-off tooling. Tracking strokes-per-die, rather than calendar time, is the more reliable way to plan tooling budgets across a year of production.
What maintenance schedule keeps uptime high?
Daily checks cover lubrication flow and ejector function; weekly checks cover die alignment and knock-out pins; a full teardown inspection every one to three months, depending on duty cycle, catches bearing wear before it causes unplanned downtime. Changeover between part families, on a well-tooled multi-station cold header, typically takes 30 to 90 minutes; plants that track this number closely tend to run noticeably higher utilization than those that treat changeover as a background cost. Energy draw varies with tonnage and stroke rate, but as a rough planning figure, mid-size frames in the 150-250 ton band draw somewhere in the 15-30 kWh range during active forming, dropping sharply during idle and tool-change periods - a detail worth asking suppliers to confirm against their own test data rather than assuming it applies universally.
Procurement checklist: RFQ, acceptance, and after-sales terms
A complete RFQ for a progressive header cold heading machine should specify part drawings, wire diameter and material, target output rate, and the acceptance standard the supplier must meet before shipment - leaving any of these out is the single biggest cause of quotation disputes later in the process.
What should go into an RFQ for a cold heading press?
- Part drawings with tolerance callouts for every head feature.
- Wire material, diameter range, and expected monthly volume.
- Required station count and target stroke rate.
- Acceptance criteria, referencing CE or ISO documentation where applicable.
- Delivery lead time and installation or commissioning scope.
- Spare parts list and after-sales response time commitment.
What acceptance standards and SLA terms matter most?
Buyers should ask for sample parts produced on the actual machine before shipment, not just a catalog spec sheet, and confirm whether CE or ISO documentation accompanies the cold heading press. On the service side, a clear after-sales SLA - response time for technical support, guaranteed spare parts (repuestos) availability, and the scope of operator training included - matters as much as the machine's rated tonnage. Plants that skip this step often find the real gap only after the warranty period starts, which is the worst possible time to discover it, and the hardest time to renegotiate terms with a supplier.
Choosing the right progressive header cold heading machine comes down to matching die stages, tonnage, and wire diameter to the actual part mix a plant runs - not to the single biggest number printed on a spec sheet. Argentine fastener producers comparing suppliers should weigh landed cost, local technical support, and documented die performance alongside the base machine price before any order is signed, since the cheapest quotation rarely stays the cheapest option once freight, duty, and after-sales gaps are added back in.
Frequently asked questions
Q: What is a progressive header cold heading machine used for?
A: It forms bolts, screws, and rivets from wire stock through multiple die stations without cutting the metal, preserving grain flow strength.
Q: How many die stations does a typical machine have?
A: Most frames run four to six stations, with simple hex bolts needing four and deep-socket heads needing five or six.
Q: What tonnage is needed for M10 bolts?
A: M10 fasteners typically fall in the 150-220 ton band, depending on head geometry and material hardness.
Q: Is cold heading cheaper than CNC machining?
A: Above roughly 5,000-20,000 pieces, cold heading usually costs less per part due to higher material yield and faster cycles.
Q: What should Argentine buyers check before importing one?
A: Confirm landed cost including duty and freight, local spare parts stock, and documented after-sales technical support before ordering.
PREVIOUS:
Get A Quote
We will contact you within one working day. Please pay attention to your email.
Latest News
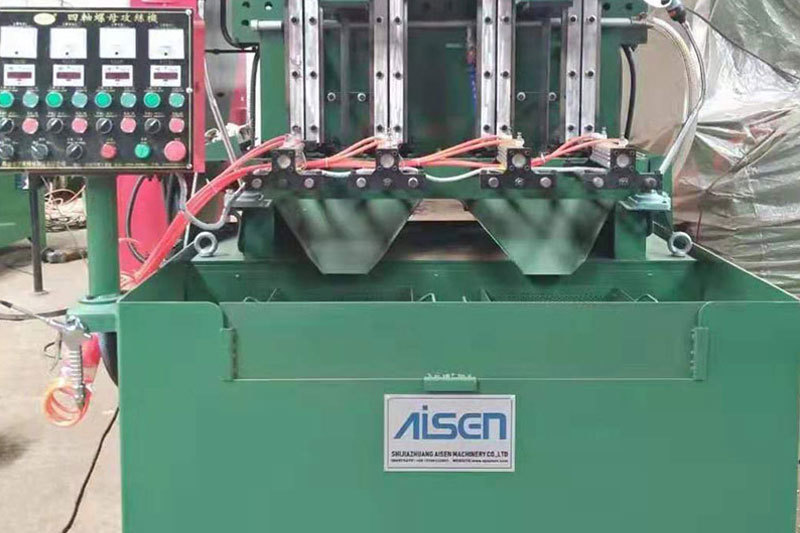
AISEN Four axis nut tapping machine ready for shipment to Russia
AISEN machinery inverted wire drawing machine
MESSAGES
We will contact you within one working day. Please pay attention to your email.
Qucik Link
Contact
Phone: +86-15100123091
E-mail: info@sjzaisen.com
Address: No.41 Zhaiying South Street, Yuhua District, Shijiazhuang City, Hebei Province China